
Concrete Block Molds
Hollow Block Mold
Solid Block Mold
Solid Brick Mold
Interlocking Block Mold
Thermal Block Mold
Author:HAWEN Block Mould Manufacturer TIME:2026-10-12
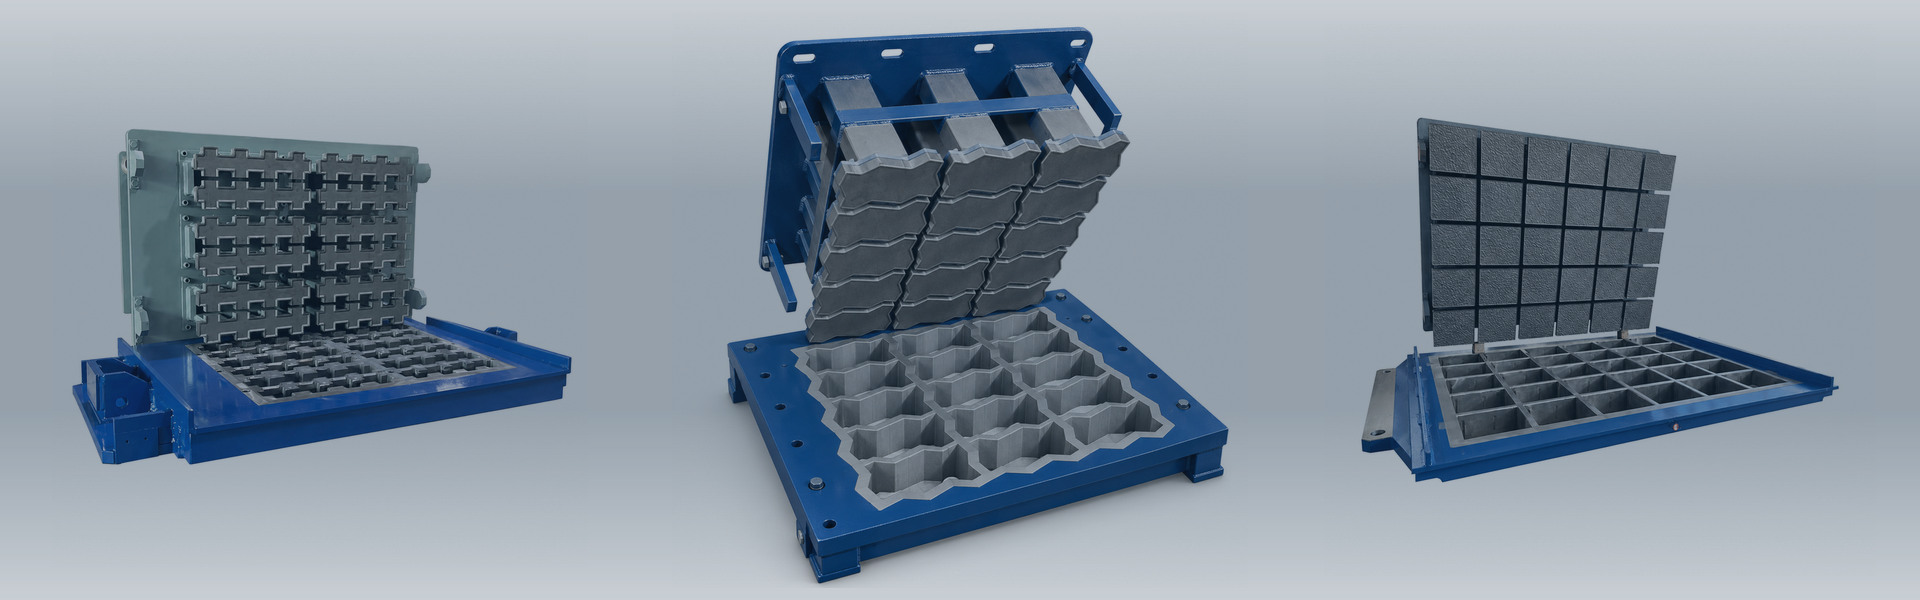
Decorative profiles, dimensions, and suitable edge details can be developed from drawings or samples. This allows the mold to reproduce the paving design selected for your product range.
Precision machining focuses on the geometry that determines how neighboring pavers align. Consistent profiles help maintain the intended appearance across larger paved areas.
Specified chamfers and special edges are reviewed during mold development. These details give the finished paver its intended outline and joint appearance.
Molds can be evaluated for production lines equipped with a face-mix system. The machine configuration and required surface-layer product are considered together during technical confirmation.
Corners, detailed profiles, and release surfaces are assessed before manufacturing. Special or newly developed designs normally undergo real-machine trials to evaluate demolding and finished shape.
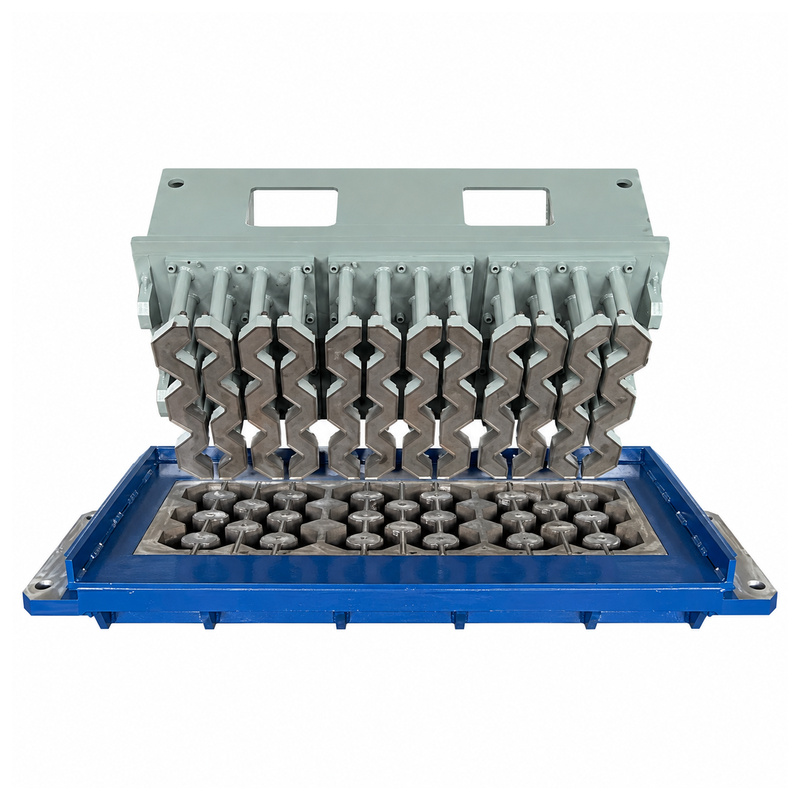
External dimensions, internal openings, and concrete ribs are developed around your grass paver design. This supports a range of grid geometries on compatible production equipment.
Opening size and concrete section thickness are evaluated together. The design review considers filling, compaction, and release requirements for the narrower sections of the paver.
Appropriate machining methods are used to reproduce core positions and internal profiles. Accurate forming components support consistent opening geometry across the product.
The complete grid shape is assessed for release from the mold. This helps address potential release difficulties that could affect fresh paver ribs and edges.
Paver dimensions, pallet area, and machine specifications determine the proposed layout. The mold is configured for your production equipment and confirmed product requirements.
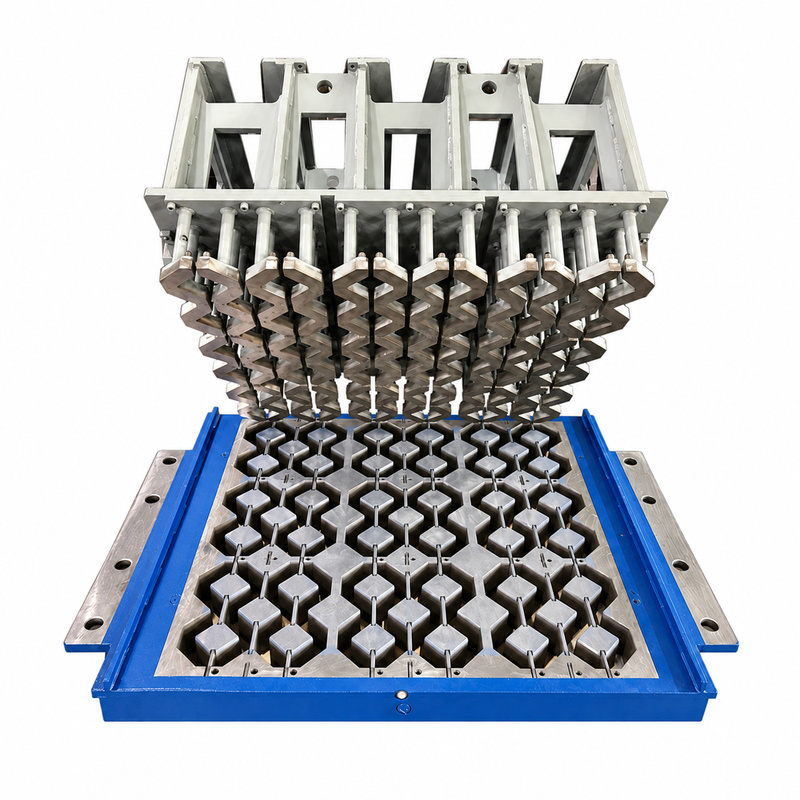
Interlocking outlines are machined to the approved product geometry. Consistent profiles help neighboring units fit together with the intended joint arrangement.
Paver thickness, chamfers, and connecting profiles can be developed according to your specifications. The final design is checked against machine capabilities and production requirements.
The specified paver mold clearance is 0.2–0.25 mm per side between the mold box and tamper head. Precision matching maintains the intended relationship between these forming components.
Suitable steel and heat treatment are applied to critical wear components. Protecting the profile surfaces helps retain the shape that determines fit between adjacent pavers.
The mold can be developed for a compatible production line with a face-mix unit. Machine details and the required paver specification are reviewed before the design is confirmed.
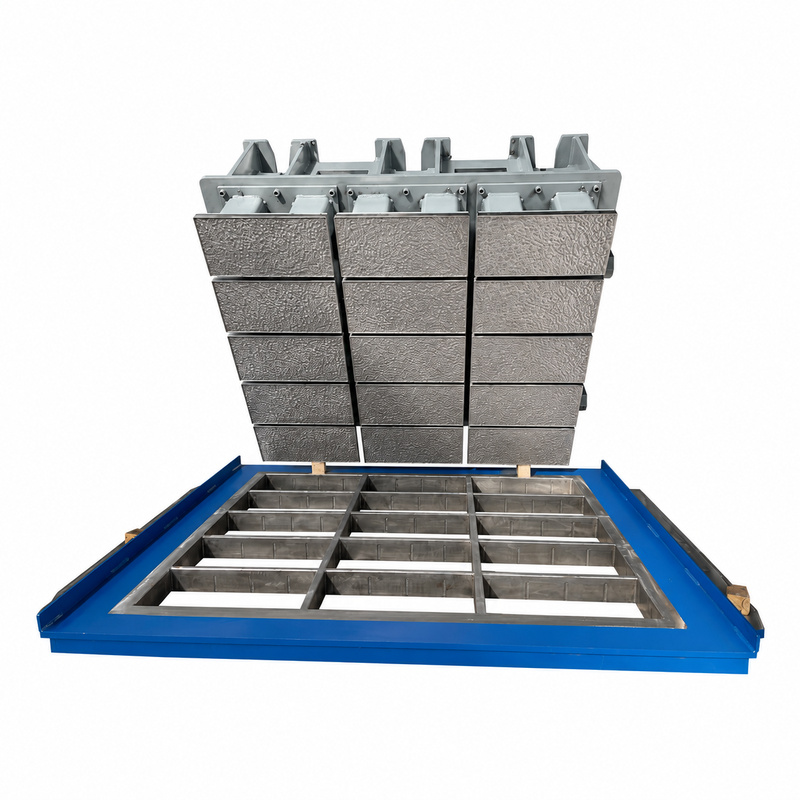
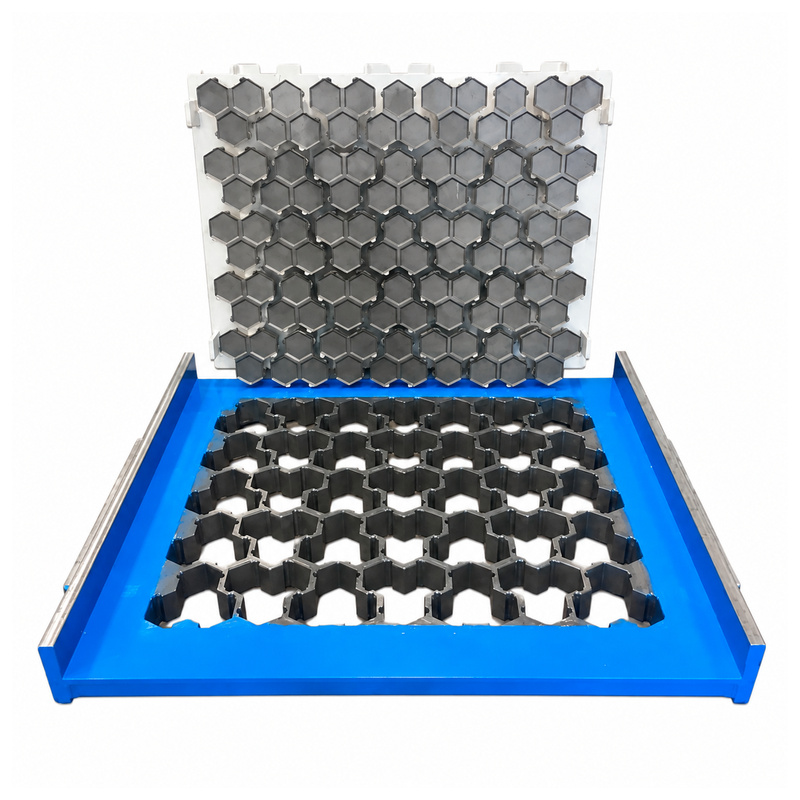
Accurate cavity machining supports repeatable rectangular paver geometry. Consistent dimensions help maintain straight joints and predictable laying patterns.
The number and arrangement of pavers are developed around the specified format and usable machine area. This provides a layout matched to your equipment.
Chamfers, spacers, and other suitable edge details can be incorporated into the mold. Drawings or samples define the features needed for the intended joint arrangement.
Critical wear components receive carbonitriding and quenching, with specified surface hardness of HRC 59–61 and an effective hardened layer of approximately 1.5 mm. Wear protection helps maintain cavity dimensions and edge profiles.
Existing paver drawings or samples can be used to develop a replacement mold. Machine dimensions and interfaces are confirmed alongside the product geometry before manufacturing.
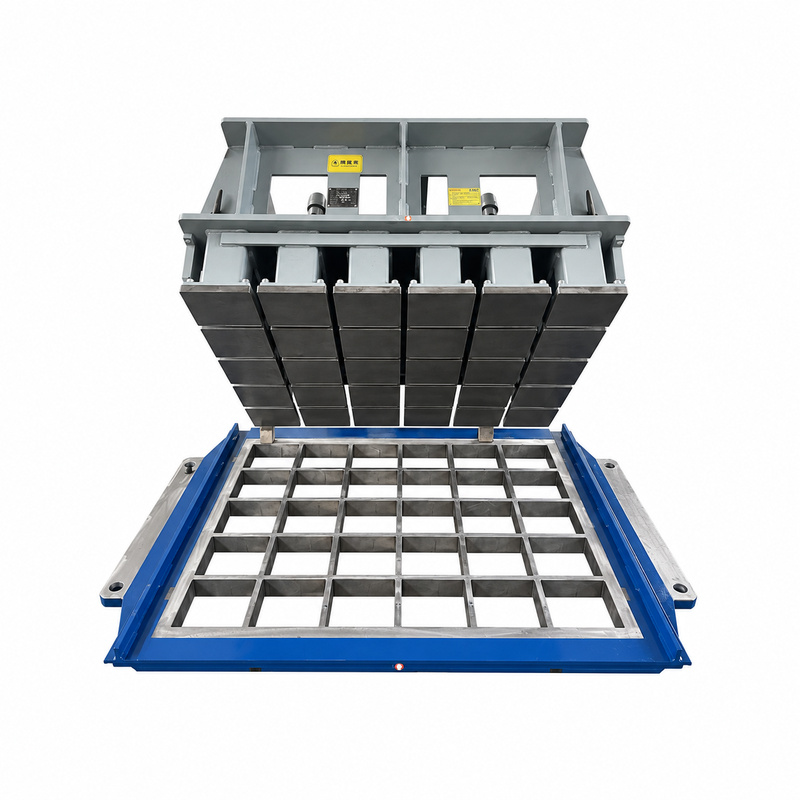
Cavity dimensions and edge profiles are manufactured according to the approved square paver design. Consistent geometry supports regular joints and alignment during installation.
Molds can be developed for different square formats and target thicknesses. Each configuration is evaluated against the working area and capabilities of your block machine.
Chamfers and suitable edge details are incorporated into the forming components. This allows the mold to reproduce the intended outline and joint appearance.
Mold development can accommodate a compatible production system with face-mix capability. The required paver and machine configuration are reviewed together before manufacturing.
Precision matching maintains the specified paver mold clearance, while suitable materials and heat treatment protect working surfaces. These measures support retention of the intended forming geometry
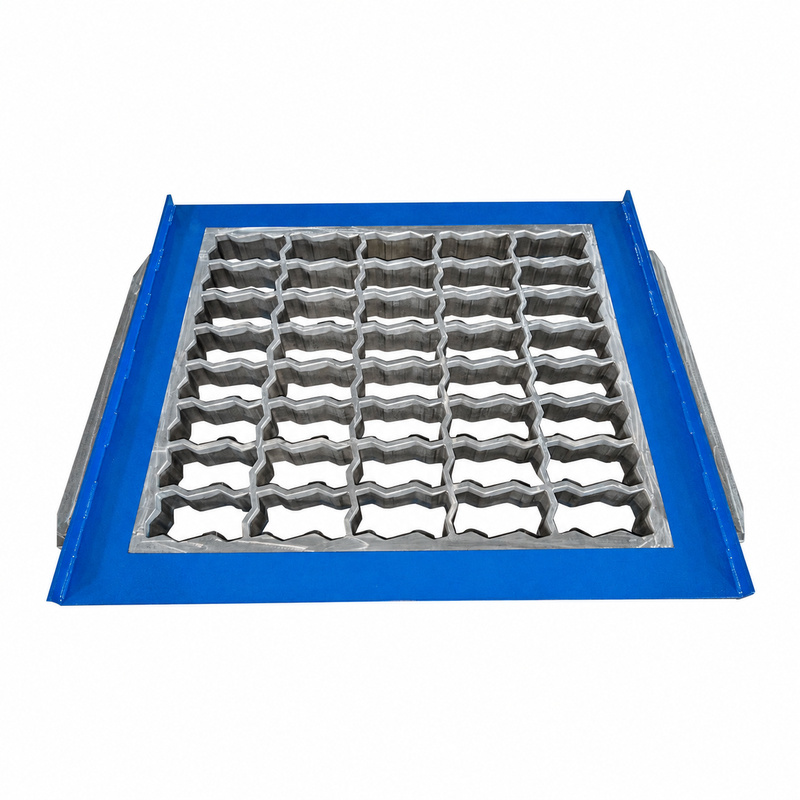
Repeated angles and connecting profiles are manufactured to your approved design. Consistent outlines support predictable fit between neighboring pavers.
Zigzag dimensions, thickness, chamfers, and suitable edge features can be developed from drawings or samples. The design is checked for production feasibility before manufacturing.
Material selection and heat treatment address the forming surfaces exposed to abrasive concrete. Protecting these areas helps preserve the detailed zigzag outline during use.
The tamper head is matched to the cavity profile and specified forming clearances. This supports consistent component alignment through the forming sequence.
An existing paver sample or technical drawing can provide the reference for new tooling. Machine and mounting information are reviewed to match both the product and production equipment.
Send the finished block drawing and machine interface details for a mould review. Explore Paver Block Molds or contact HAWEN to discuss the required tooling.

 Tel: +8618359454595
 Email: sale@hwmachines.com
 MP/WhatsApp: +8618359454595
 Manufacturer Address:Nanan, Quanzhou City, Fujian Province, China




